UT Quality USA fields union NDT crews for pipeline, midstream, and industrial construction — the complete conventional and digital NDT suite, led by our proprietary UT Scan automated ultrasonic technology, with technicians certified to SNT-TC-1A / ANSI/ASNT CP-189.
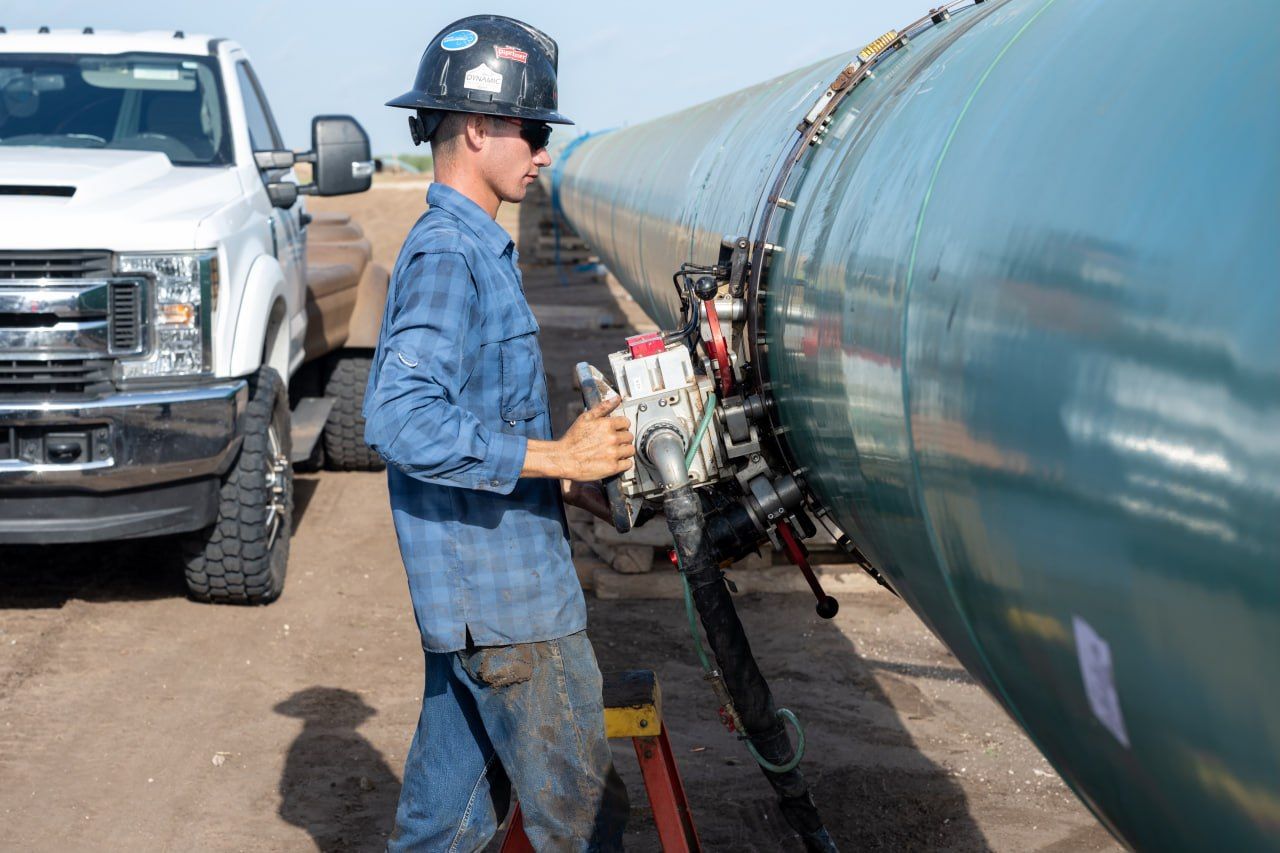
UT Quality USA is a union NDT operation. For pipeline and energy owners running union labor — or projects under a Project Labor Agreement — our crews can be staffed on the same labor basis as the rest of the spread.
Union technicians, certified to SNT-TC-1A / ANSI/ASNT CP-189, who fit cleanly onto union mainline and station work under owner and contractor labor agreements.
Trained and certified to our written practice, and working to standardized written procedures on every spread.
Encoded, recordable AUT data and full interpretation records that stand up to audit — acceptance decisions the owner can defend.
UT Quality USA delivers the complete range of nondestructive testing — from automated ultrasonics to surface methods, with in-house Level II/III interpretation — plus in-field welder qualification testing and independent Level III auditing and review.
Advanced NDT
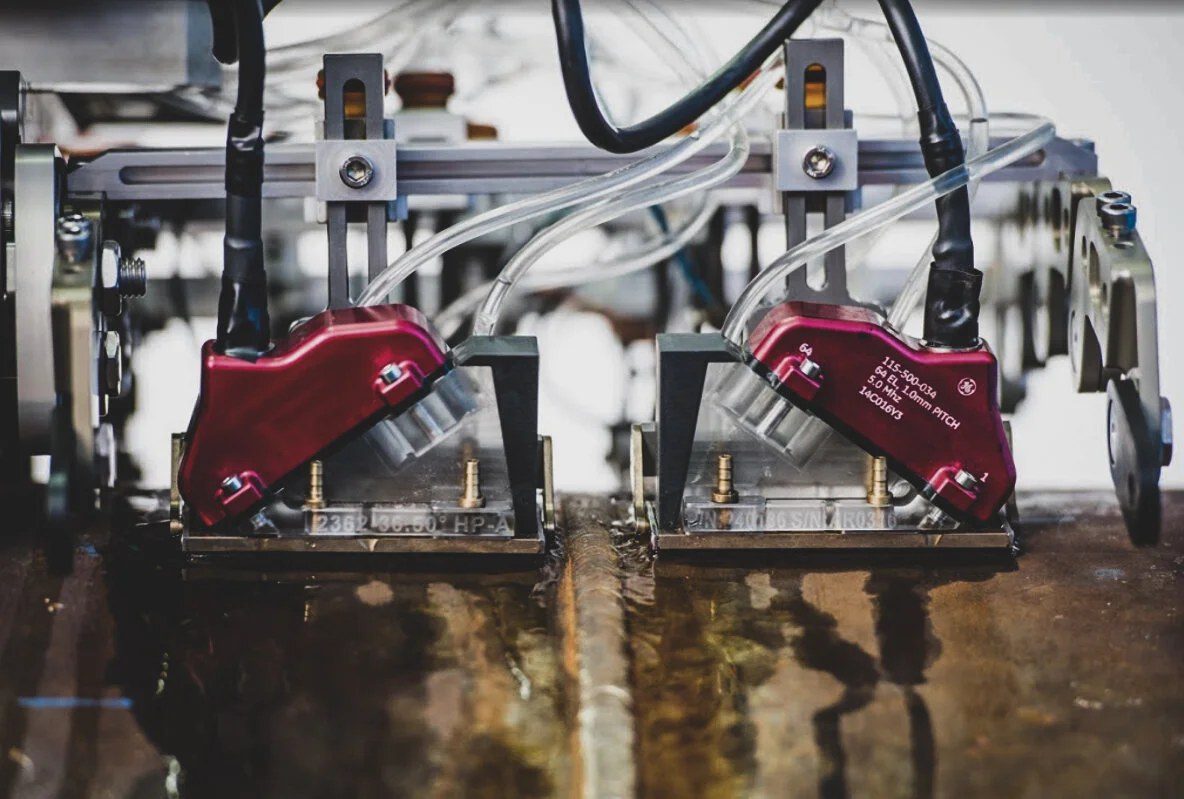
Proprietary UT Scan AUT — zonal phased array (PAUT) with TOFD — for fast, repeatable, fully encoded girth-weld inspection on pipeline construction. Full AUT spreads for mainline construction, with production-rate coverage and a defensible record. Automated ultrasonic testing →
Encoded phased array and TOFD for girth welds, process piping, vessel seams and nozzles — plus semi-automated UT on a hand-driven scanner for tie-ins, repair welds and fittings. Phased array UT & TOFD →
Direct radiography (DR) with an X-ray tube or an isotope source, computed radiography (CR), real-time radiography (RTR), flexible detector panels and crawler systems — an interpretable image at the weld, with no darkroom. Digital radiography →
The NDT portion of the integrity dig: phased array corrosion mapping, remaining wall thickness, pit depth, C-scan corrosion maps and 3D laser mapping, documented for your engineering team. Integrity & corrosion mapping →
Conventional NDT
Conventional film RT where it is specified, alongside DR, CR and RTR, interpreted to API 1104, ASME B31 or ASME Section V/VIII. Radiographic testing →
Magnetic particle, liquid penetrant, manual ultrasonic thickness and flaw detection, and visual testing — plus positive material identification (PMI). Conventional NDT →
In-house Level II technicians, Level III oversight, and remote Level III interpretation for fast, qualified acceptance decisions.
Weld & program services
Girth-weld inspection on new construction by AUT or radiography, tie-ins and station piping, qualification support and repair-weld verification. API 1104 weld inspection →
Welder qualification at the job site. A destructive test: coupons are cut from the test weld, bend and tensile tested, then examined by our AWS Certified Welding Inspector (CWI), who approves or rejects the qualification to the project’s welding code. In-field welder testing →
Independent Level III procedure review, film review of radiographic film and CR/DR images, and PHMSA audit review of inspection records to help operators prepare for a PHMSA audit. Auditing & review →
Legacy RT weld film converted to searchable digital weld records in the DICONDE format, indexed to job, line and weld, with a documented chain of custody. Film digitization →
UT Quality is not PHMSA and does not act for PHMSA; we hold no PHMSA certification, approval or authorization and do not determine compliance. Audit review is an independent Level III review of your procedures and records to help you prepare.
Our phased-array and automated ultrasonic systems put encoded, recordable data behind every girth weld — faster than film, and with a defensible digital record the owner can audit.
Deep-dive resources on the methods behind UT Quality’s work — the technology, the codes, and the decisions that put the right method on every weld.
AUT / PAUT
How an encoded scanner reads a girth weld zone by zone — and clears it without film.
Explore AUT →Radiography
Exposure by diameter plus 45 minutes of darkroom — add it in and digital is 5–48× faster to a decision, every size.
See the comparison →Heavy wall
RT exposure and source energy climb with wall thickness; AUT/PAUT scan time rises far more gently — typically 5–10 minutes a weld.
See the chart →Method selection
A clear decision flow for when RT is still right and when ultrasonics should be primary.
See the decision flow →Two different things, kept distinct: the codes and standards a project is inspected to, and the certifications our personnel hold.
Codes & standards we work to
Personnel certifications
Level I, II and III personnel qualified and certified under the employer’s written practice — to SNT-TC-1A and/or ANSI/ASNT CP-189, per the applicable written practice and project requirements.
Level II and Level III technicians trained and qualified in-house — the same interpretation standard on every crew and every spread.
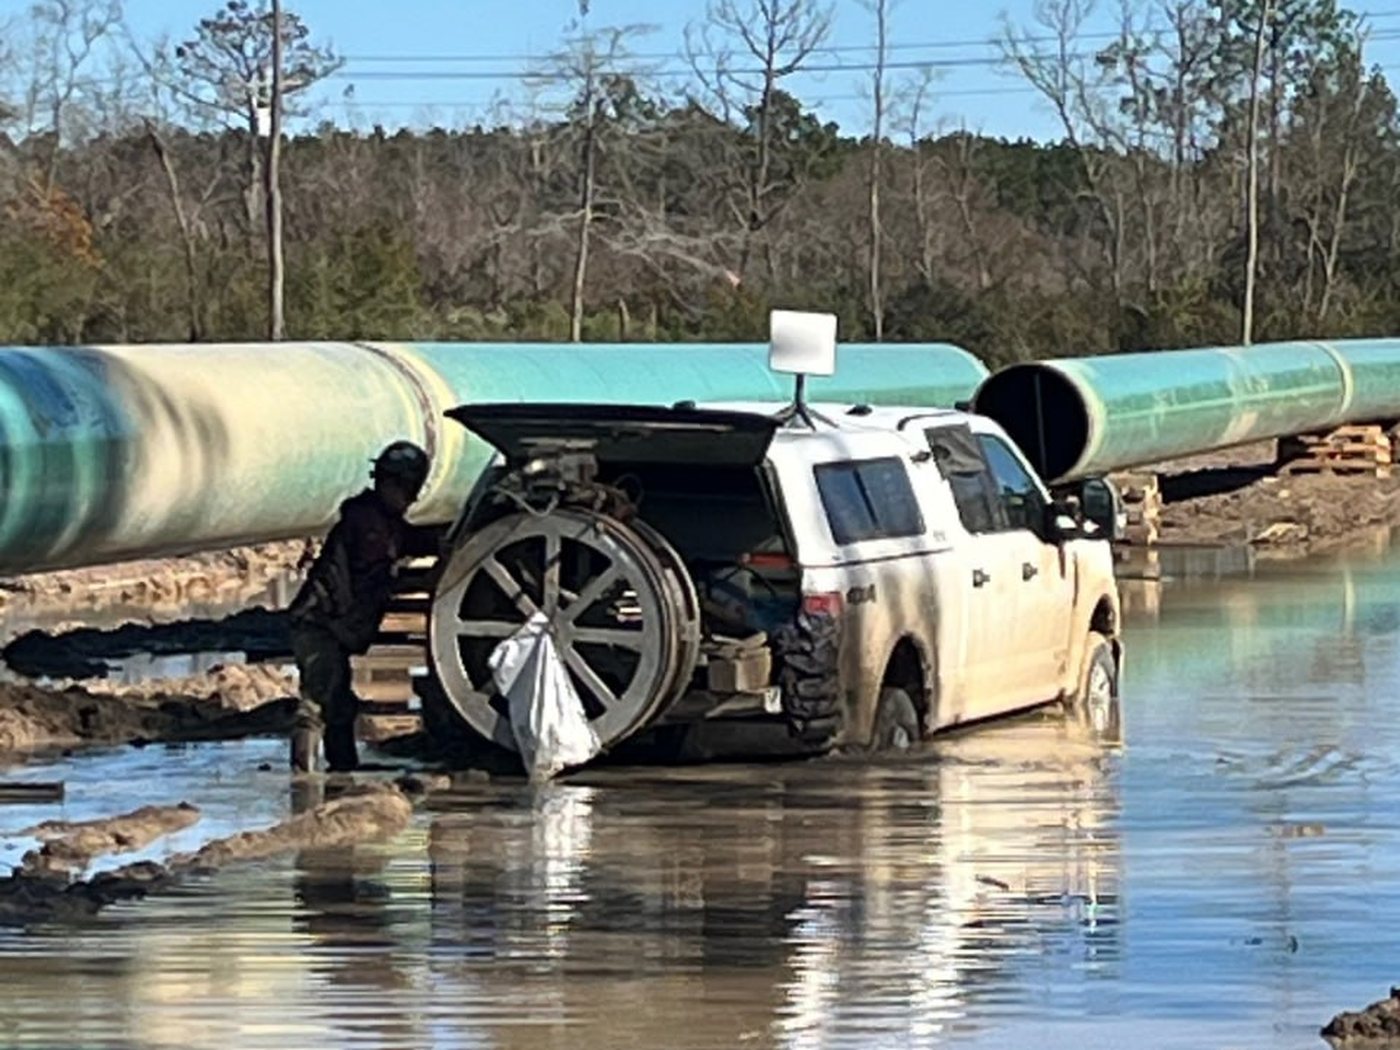
UT Scan is our own automated ultrasonic system — not rented, not licensed. We build, maintain, and advance it, so the field crew and the technology answer to one company.
Standardized written procedures and a single written practice, with Level III oversight, keep interpretation consistent from spread one to spread ten.
Union crews, certified to SNT-TC-1A / CP-189, staffed onto union projects and PLAs on the same labor basis as the rest of the job.
More than two decades — inspecting onshore, offshore and industrial energy assets across North America and on international projects since 2003.
UT Quality’s work is on the record — a documented history of onshore and offshore projects since 2003, from large-diameter transmission mainline to offshore tie-ins.
Most of the work is large-diameter transmission line — 30″ to 56″, with 42″ and 36″ the most common. Our largest deployment ran up to 45 crews across nine spreads on a single project (Mountaineer XPress, Columbia Gas Transmission).
Operators served
UT Quality USA mobilizes to pipeline and industrial projects nationwide from our Katy, Texas base.
U.S. union NDT services with the ability to support pipeline, facility, industrial, spoolbase, and offshore projects.
Katy, Texas — corporate HQ, project management, training, qualifications, spares, and equipment maintenance in-house.
Crews and equipment mobilized to project sites nationwide — crews scaled to the project, up to 45 on our largest deployments.
Tell us about the project and scope — a UT Quality representative will follow up.
UT Quality USA operates from the Katy, Texas headquarters it shares with RAE Energy.
The RAE family of companies